25–30%
time saved on troubleshooting
Provably lower MTTR.
Mean time to repair gets shorter, and the difference shows in OEE. Numbers you can defend in a quarterly review without hand-waving about "improving processes."
Edmund is an AI debugging platform that reads your PLCs, HMIs, schematics, manuals, alarms, and maintenance journals. Unifies all of your data sources into one platform with a reliable maintenance workflow.

Searching „servo drive enable“ in programs
Found the servo control block FB 1343 Faulhaber MCBL. The drive is enabled when it is online, not cancelled, and a motion command (Home / Jog / Positioning) requests it.
#GoHallZero starts it only while neither #Cancel nor #Stop is set, line 143. #status.enabled is off, it first sets #state.enable.start, lines 144 to 145.  S7-1500 · ET200MP
142//Go Hall Zero143IF #GoHallZero AND NOT #Cancel AND NOT #Stop THEN144 IF NOT #status.enabled THEN145 #state.enable.start := true;146 END_IF;147 #state.goHallZero.start := true;148 #status.done := false;149END_IF;
Searching „R1 waits at the pick“ in robot programs
R1 is waiting in plcWaitVacuum for its vacuum switches. It stays at the pick until diVacuumReachedModules12 is on, and diVacuumReachedModules34 too when it picks with both circuits, line 66.
doRobAtPick is on and doRobMoving off, lines 64 to 65. doRobAtPick drops and doRobMoving comes back, lines 67 to 68.  IRC5 · T_ROB1
62PROC plcWaitVacuum(bool bBoth)63 ! the switches of the circuits it switched on64 SetDO doRobMoving,0;65 SetDO doRobAtPick,1;66 WaitUntil diVacuumReachedModules12=1 AND (NOT bBoth OR diVacuumReachedModules34=1);67 SetDO doRobAtPick,0;68 SetDO doRobMoving,1;69ENDPROC
Searching „-94B1“ in documents
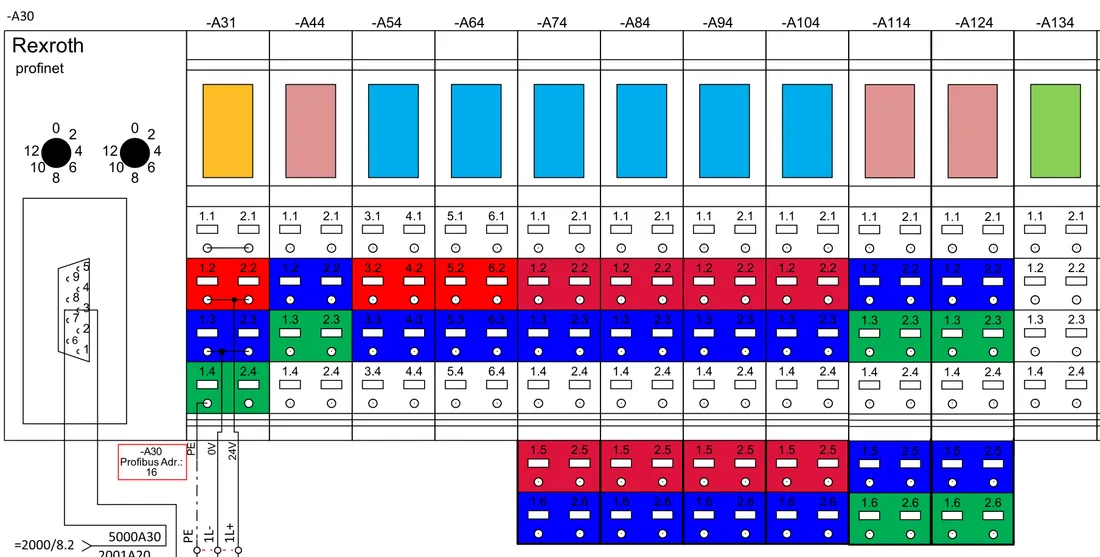
-94B1 is the product-detect photocell (SICK WL12-2P430) on conveyor 3.
It’s wired to input %I4.3 on DI module -A4, through terminal X1:11–12 in cabinet +SK3.
Querying „energy_by_state“ for IMM01, Jan 12–18, 2026
Pulled IMM01 power from the MES historian for Jan 12–18, 2026 and bucketed it by machine state:
The machine drew power while idle for 74 h, more than double its 31 h of actual production. Trimming idle time is the fastest saving here.
1SELECT state, ROUND(COUNT(*) / 4.0) AS hours2FROM energy_by_state3WHERE machine = 'IMM01'4 AND ts >= '2026-01-12' AND ts < '2026-01-19'5GROUP BY state6ORDER BY hours DESC;
| State | Hours |
|---|---|
| ON_NO_PROD | 74 |
| OFF | 63 |
| PROD | 31 |
Searching „photocell cleaning interval“ in documents
Clean the photocell lenses every 240 operating hours. That is the interval in the conveyor 3 manual, rev 04/2024.
Your maintenance log shows the lens was last cleaned 312 h ago, past the 240 h interval. That lines up with the repeated photocell dropouts.
“Clean the lenses of all photocells in the infeed section every 240 operating hours. Dust on a lens causes dropouts on the product-detect signal.”
Description
Photocell -94B1 dropped out twice in one shift. Cleaned the lens and the reflector; the signal held for the rest of the shift.
Searching „Station 52 photocell“ in maintenance journals
Yes. The Station 52 photocell replacement (Tomáš Marek, Apr 23) sits at the top of the Line 4 journal, indexed alongside every recent fix:
Open any entry for the full symptom, cause and fix. The next technician inherits it instead of rediscovering it.
Description
The photocell at the Station 52 transfer stopped seeing pallets after a pallet knocked its bracket. Parts piled up at the transfer.
Solution
Replaced the photocell with the same type, aligned it to the reflector and ran 50 test cycles without a dropout.
Reading the dashboard of Assembly line 4
Assembly line 4 is fully indexed and every source is active:
A plant lead can confirm coverage at a glance and catch a source that’s gone stale before someone hits the gap mid-fault.




An hour of unplanned downtime on a tier-2 automotive line.
We bet your last downtime took more hours than you would have liked.
Mean time to repair gets shorter, and the difference shows in OEE. Numbers you can defend in a quarterly review without hand-waving about "improving processes."
An ordinary technician picks up where a PLC specialist used to be needed.
Every fault has a documented root cause. The board review stops being "we're working on it" and starts being "this is the third Tuesday relay sticking; here's the procurement plan."
When a line stops, the problem usually isn't the repair itself — it's diagnosing the right problem. Your data already has the answer, scattered across PLC projects, schematics, alarms, journals, and people's heads, but none of it connects. Edmund significantly shortens the diagnostic step.
Across our deployments, the part swap is rarely the bottleneck. The hour you lose is upstream, figuring out which part, why it failed, and whether it'll come back next quarter.
PLC projects, EPLAN drawings, alarm history, maintenance journals, and what's only in the head of the senior technician — separate systems, separate handoffs, no map between them.
A traceable answer beats a confident guess. Edmund hands the technician the cause and the next step, with citations, so the only thing left to do is the wrench work.
Maintenance knowledge sat in three places, hundreds of PDFs, handwritten logs, and the heads of technicians who'd spent decades on the floor. None of it was searchable. Edmund pulled all of it into one query box.
A junior technician answering a 2 a.m. fault alarm now reaches the same institutional knowledge a senior engineer could recall in seconds. Adoption was immediate, the interface was simple enough that technicians started using it on day one without prompting.
The standout feature was voice input. Instead of typing notes after a long shift, technicians dictate directly on the floor and Edmund writes the entry into the digital maintenance log automatically.
At its Bojkovice plant, Moravia Cans uses Edmund to support fault diagnosis and repair preparation. The company makes aluminum aerosol cans on high-speed forming and printing lines and has grown by 60% over the past three years.
Maintenance technicians can consult equipment documentation, review previous maintenance interventions and check spare parts availability through a single interface.
Alongside manuals and maintenance records, they can access operational data held in the plant's business systems, Microsoft SQL Server and the QAD ERP, without writing SQL queries or navigating database structures.
Technical documentation at Model Obaly was split across shared drives, service systems, inventory records and paper binders. Edmund helped digitise the paper documentation and connected all the sources in one interface that maintenance technicians can use right at the machine.
Edmund became the common starting point for diagnosis right at the machine. A maintenance technician talks the fault through with the system and can learn the root cause within a few seconds. If a spare part is needed, they find out straight away whether it is in stock and go to get it without a stop at the workshop. Instead of needless walking, switching between systems and phoning colleagues, they have the answer at hand.
References from our customers
Now we have everything in one place, right at the machine. I enter the details of a fault and within a few seconds I see what it means, how it was solved in the past and whether we have the parts if we need them. I don’t have to switch between systems or look anything up. Finding root causes is faster, and when we use the system we have the potential for shorter breakdowns, on average by up to 30%. For me, the biggest benefit is that people can focus on the repair, not on searching for information.
AI is the only tool that can systematically work with data from multiple sources. Using Edmund has led to a lower frequency of a specific failure, or even its complete elimination.
We've had a very positive experience with Edmund. The results have an immediate impact on the efficiency of our production processes.
New production lines and machines are coming to our plant, and we don't yet have the experience to diagnose them efficiently. At the same time, we can't grow the maintenance team to keep up. So we use Edmund AI as an "invisible co-worker": it fills the missing know-how, supports our technicians' decisions, and speeds up finding and fixing faults.
Industry 4.0 promised a lot but delivered very little. Edmund is genuinely making a difference.
Edmund links your PLC programs, schematics, robot programs, documents, live data and maintenance journals into one graph.
FB_Cell11_Safety, line 48. %I4.3 is the safe run permit: when it drops, cell 11 stops.


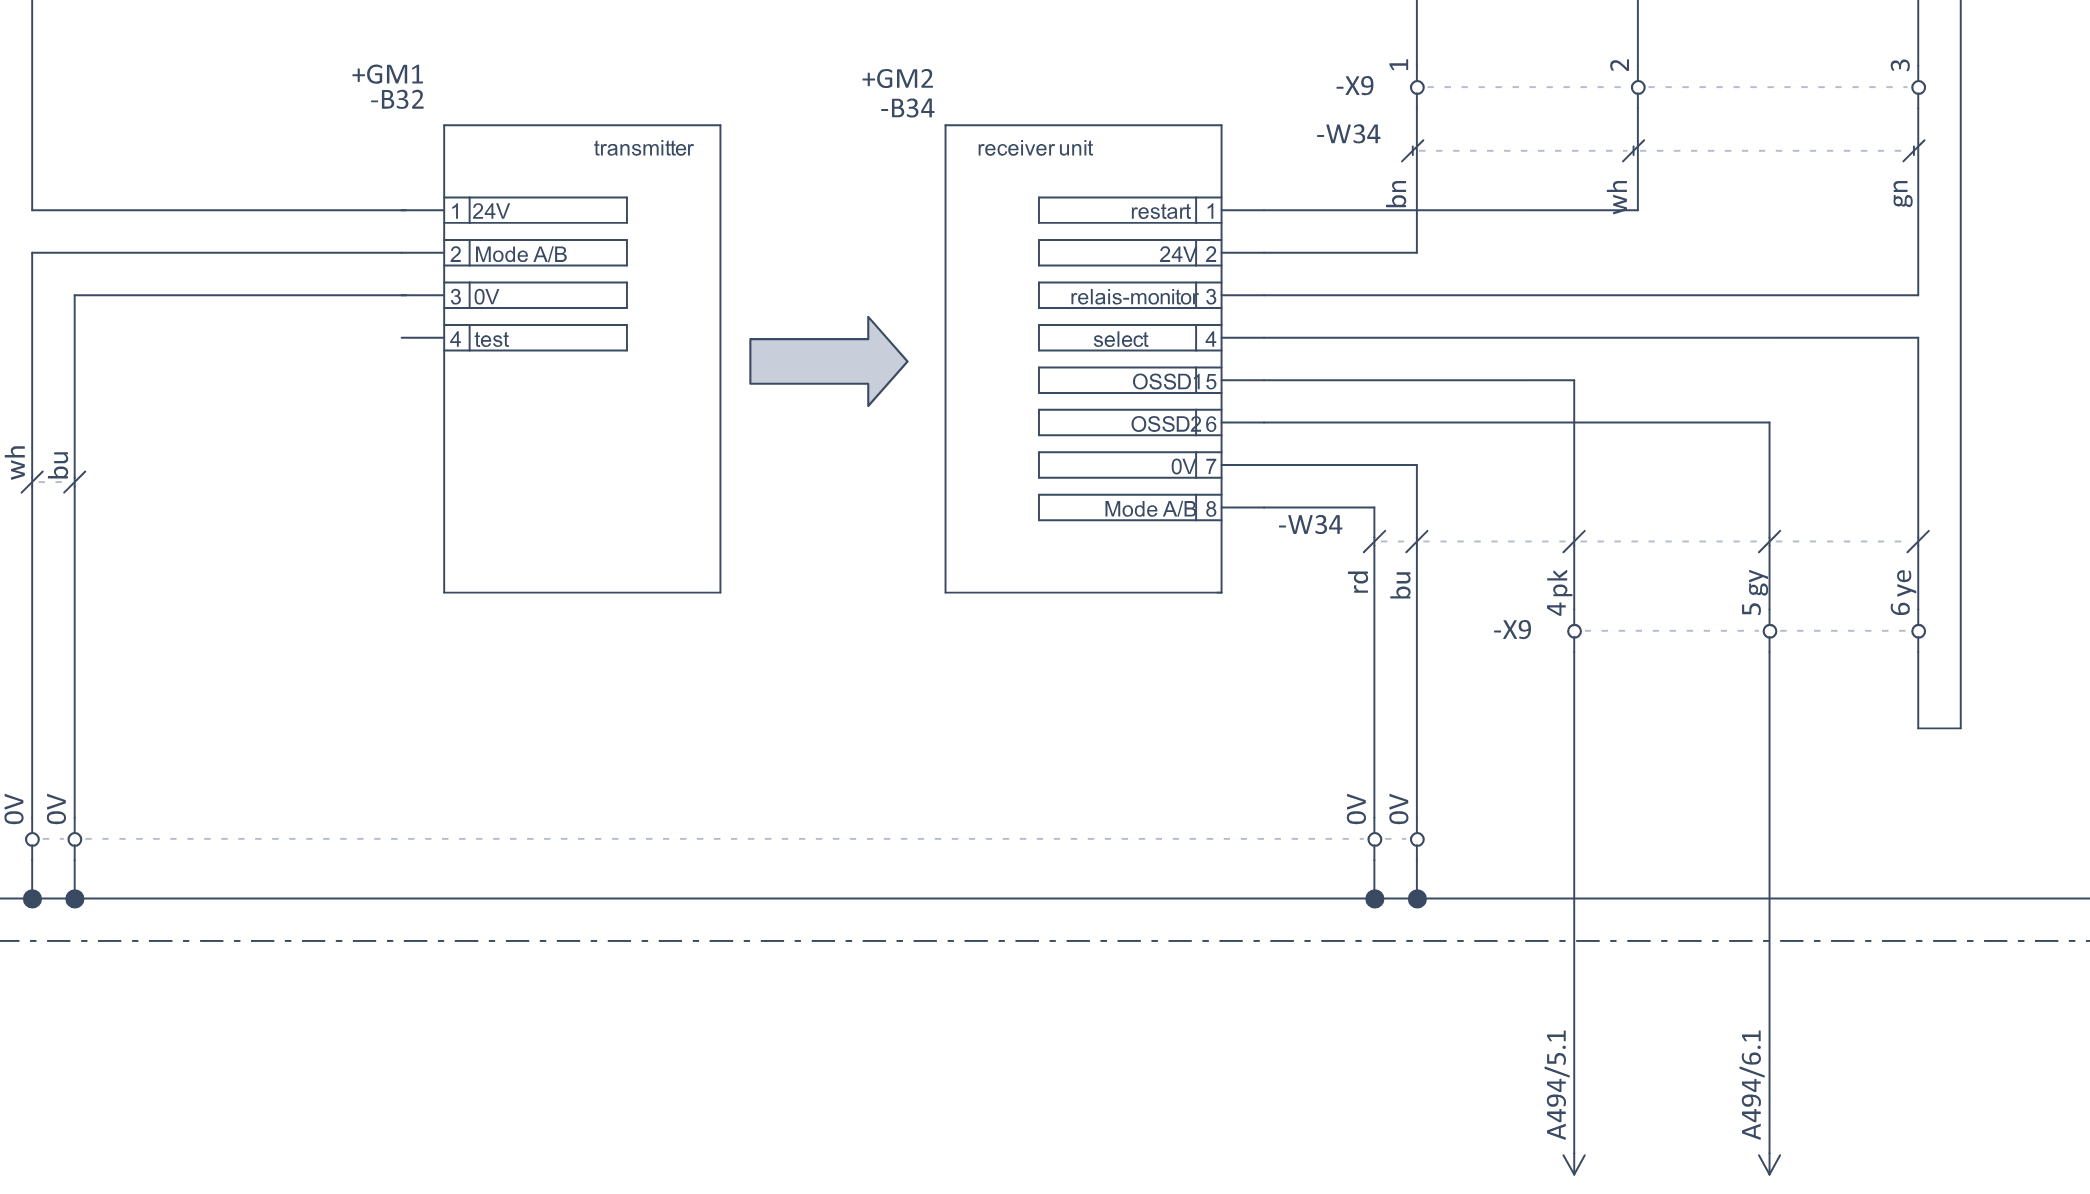
%I4.3 leads to EPLAN sheet 217: the light curtain receiver -B34, wired through terminal X9:4.
The ABB robot in cell 11 reads di_VariantB at line 85: variant B loads at pLoadB with gripper G2.
Third safe stop in 30 days, all on night shift. Gripper G2 was replaced and pLoadB re-taught on 12 April.
That’s -B34, the light curtain receiver at cell 11’s loading station.
Its OSSD1 output feeds %I4.3, the safe run permit in FB_Cell11_Safety, line 48.
All three stops came during variant B, which only runs on night shift.
Variant B loads at pLoadB, re-taught when gripper G2 was replaced on 12 April. It now sits 38 mm closer to the loading station, so the gripper’s air hose cuts the curtain’s beams.
Re-teach pLoadB clear of the protective field. Then re-route the air hose on gripper G2.
This project was realised via financial support from Technological Incubation program